Access Floors
Raised access floors help create the perfect indoor environment by maintaining high-quality clean air, improving personal comfort control, and responding to organisational and technological changes quickly and cost-effectively.
Data centres can benefit from access floors by providing a pre-engineered flexible solution to separate and organise different types of services while maintaining easy access to add and reconfigure equipment.
ConCore 800
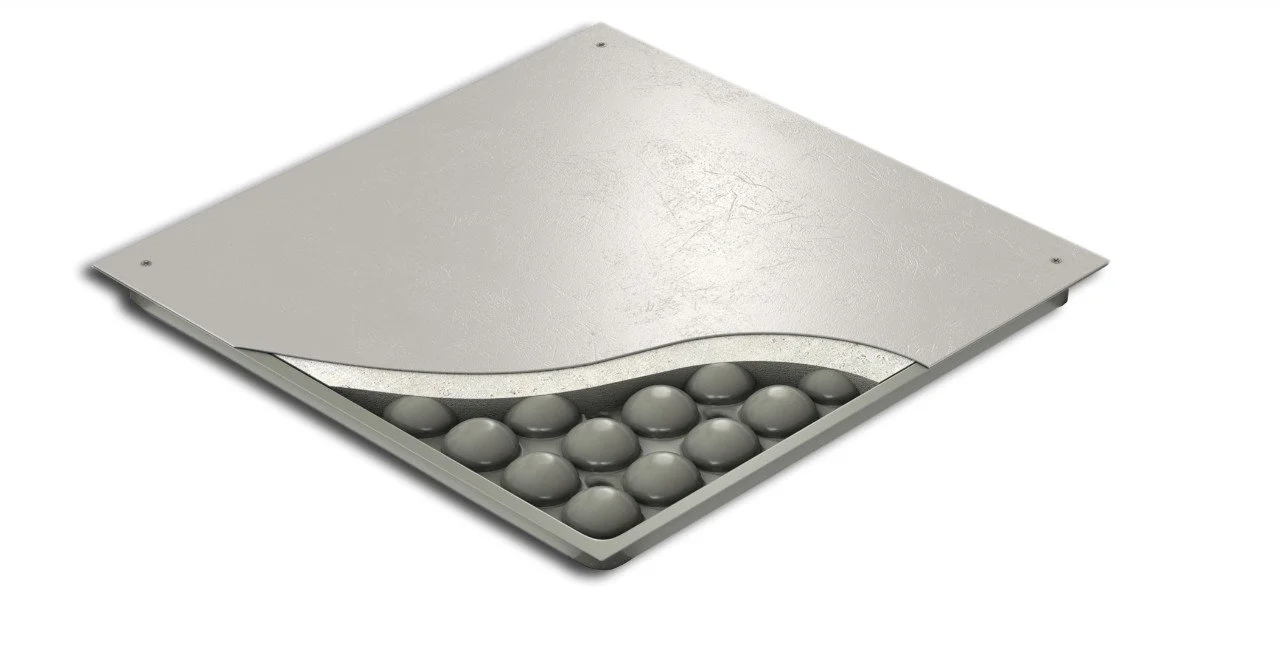
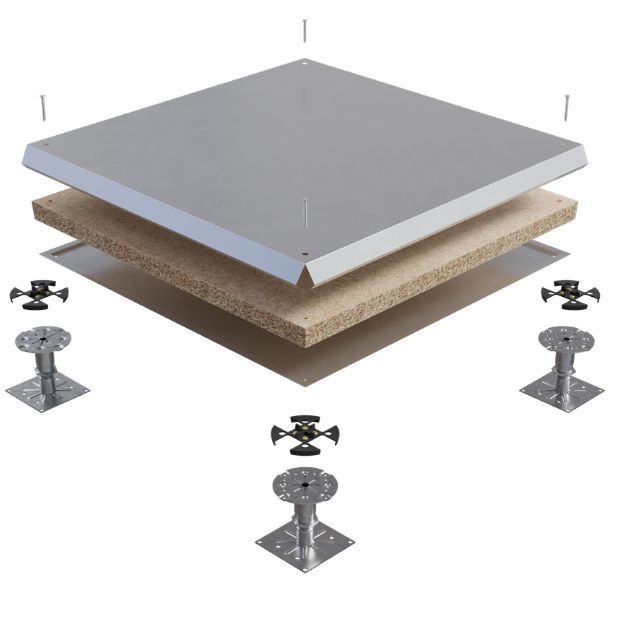
Tate's ConCore® 800 raised access floor panel is intended for light-duty commercial applications with a total load requirement of 800 lbs or less and is engineered to meet Tate Standards per CISCA testing methods.
-
Panel weight: 37.7 kg/m² bare
All steel welded construction filled internally with a cementitious core material
Protected from corrosion by an epoxy paint finish
Class A flame spread rating
Non-combustible material
-
ConCore 1500
Tate's ConCore® 1500 raised access floor panel is intended for commercial applications with a total load requirement of 1000 lbs or less and is engineered to meet Tate Standards per CISCA testing methods.
-
Panel weight: 44 kg/m² bare
All steel welded construction filled internally with a cementitious core material
Protected from corrosion by an epoxy paint finish
Class A flame spread rating
Non-combustible material
-
ConCore 4000
Tate's Concore® 4000 raised access floor panel is intended for commercial applications with a total load requirement of 17.8kN or less and is engineered to meet Tate Standards per CISCA testing methods.
-
Panel Weight: 23.9kg
All steel welded construction filled internally with a cementitious core material
Protected from corrosion by an epoxy paint finish
Class A flame spread rating
Non-combustible material
Understructure: Bolted Stringer system
-
ConCore 1000
Tate's ConCore® 1000 raised access floor panel is intended for commercial applications with a total load requirement of 1000 lbs or less and is engineered to meet Tate Standards per CISCA testing methods.
ConCore 2000
ConCore 2000
Tate's ConCore® 2000 raised access floor panel is intended for commercial applications with a total load requirement of 2000 lbs or less and is engineered to meet Tate Standards per CISCA testing methods.
-
Panel weight: 50 kg/m² bare
All steel welded construction filled internally with a cementitious core material
Protected from corrosion by an epoxy paint finish
Class A flame spread rating
Non-combustible material
-
-
Panel weight: 35 kg/m² bare
All steel welded construction filled internally with a cementitious core material
Protected from corrosion by an epoxy paint finish
Class A flame spread rating
Non-combustible material
-
ConCore 3000
Tate's ConCore® 3000 raised access floor panel is intended for commercial applications with a heavy total load requirement and is engineered to meet Tate Standards per CISCA testing methods.
-
• Panel weight: 39.3 kg/m² bare
• All steel welded construction filled internally with a cementitious core material
• Protected from corrosion by an epoxy paint finish
• Class A flame spread rating
• Non-combustible material
-
Bolted Stringer
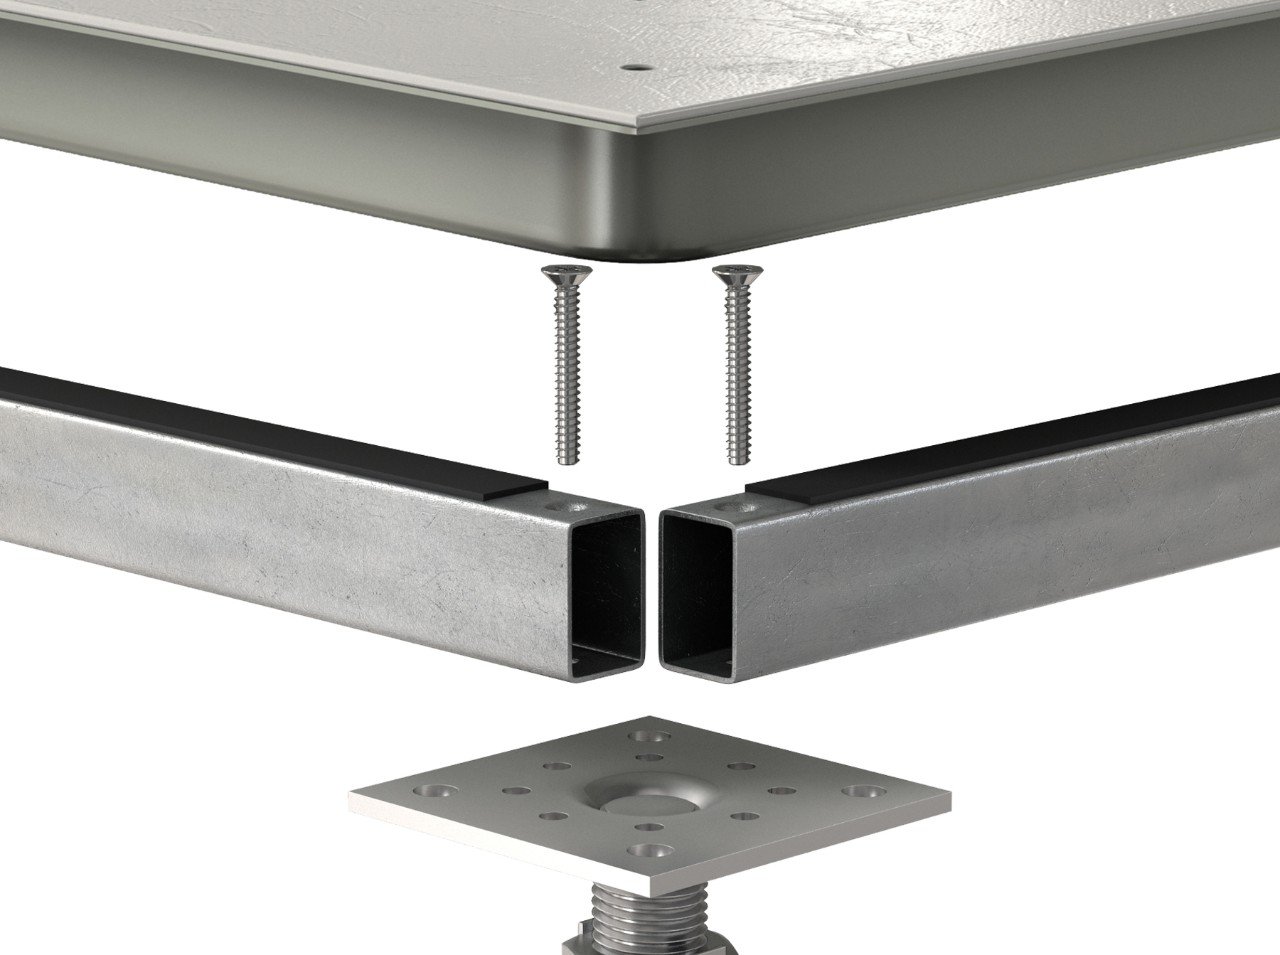
The Bolted Stringer system provides lateral resistance to heavy rolling loads & seismic loading.
-
Panels can be gravity-held in understructure for fast removal and replacement
Stringers provide lateral resistance to heavy rolling loads and seismic loading
Seismic force-resistant pedestal are available to limit or eliminate the need for special bracing
Allows floors to be built over 24" high
Typical floor heights from 12"-36"; low finished floor heights (LFFH) available from 2.5"-4"
2 inch deep stringers are available for additional loading needs
RMG600+
RMG600+ Our lowest ever embodied carbon access floor
Tate RMG600+ part of the Lower Embodied Carbon (LEC) range is a market first for access floors. Produced using a minimum of 91% recycled content and low carbon steel, this latest AS 4154-1993 approved raised access floor panel, also comes with a full 25-year warranty. Ideal for demanding commercial office environments requiring low embodied carbon and high-performing solutions.
-
Minimum of 91% recycled content
17 Responsible Product Value (RPV) contribution under Green Star
Only Genuine Lower Embodied Carbon Raised Access Floor on the Market
AS 4154-1993 approved
25-Year Total System Warranty
-
Seismic Understructure
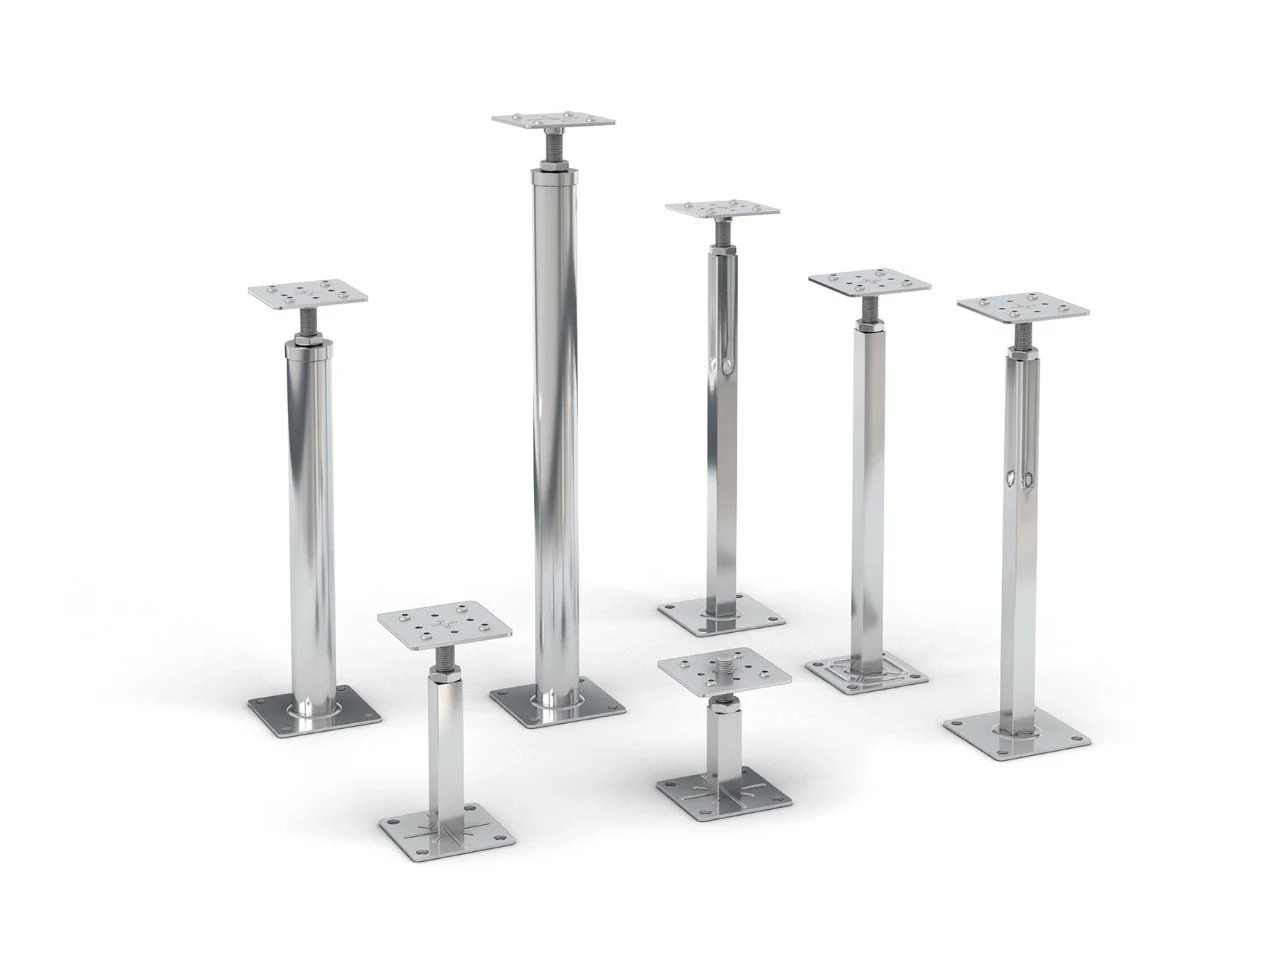
Tate offers a wide range of understructure that can withstand a variety of seismic standards.
-
• Availble in multiple floor heights
• Meets all CISCA standards
• Can limit or eliminate the need for special bracing

Cornerlock
The Posilock understructure system provides self-engagement and positioning of the raised floor panels without the need for stringers.
-
• Provides self-engagement and positioning of floor panels
• Self-capturing fastener remains within the panel and will not get lost
• Steel pedestal head provides maximum strength
• Pedestal nut provides anti-vibration and locking features
• Seismic force-resistant pedestals are available that limit or eliminate the need for special bracing
• Typical floor heights from 5”-24”; low finished floor heights (LFFH) available from 2.5"-4"